

Qingdao Senlida Packing Co., Ltd. is one of the most reliable manufacturers and suppliers of high barrier back seal pouches in China. With abundant experience, we warmly welcome you to buy bulk durable high barrier back seal pouches from our factory. Good service and quality products are available.
PRODUCT FEATURES
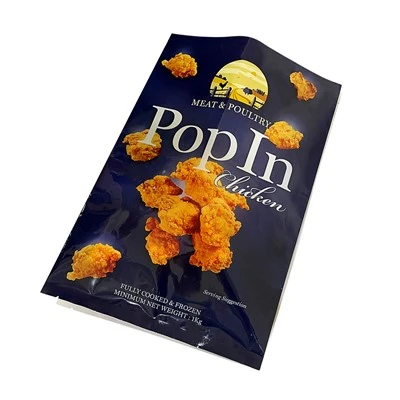
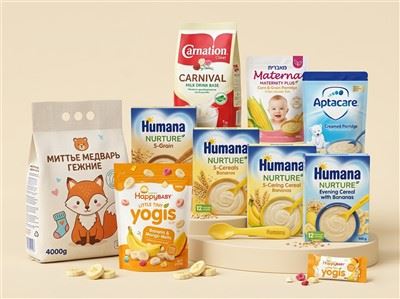
High barrier back seal pouches are functional flexible packaging solutions that provide exceptional protection against oxygen, moisture, and aroma loss. They are specifically designed for high-value products that demand strict storage conditions and extended shelf life. These pouches are widely used in specialty coffee, fresh meat products, baked goods, pharmaceutical intermediates, and other sectors.
Constructed with multi-layer composite structures, high barrier back seal pouches can be precisely engineered to include EVOH high-barrier layers, nylon puncture-resistant reinforcement layers, and aluminum or metallized light-blocking layers according to product requirements. This combination effectively prevents the ingress of oxygen, moisture, and ultraviolet light, while preserving the product's aroma and protecting active ingredients from oxidative degradation. Under ambient conditions, such packaging can significantly extend product shelf life, while reducing customers' cold chain transportation and storage costs.
The pouch body features a full-length central back seal, eliminating weak points along the edges. The heat seal is uniform and stable, ensuring leak-proof performance. Meanwhile, the front surface remains free of seals, providing a smooth, uninterrupted plane that maximizes branding and marketing opportunities, while maintaining protective performance and shelf display appeal.

CUSTOMIZATION OPTIONS
Our high barrier back seal pouches can be equipped with auxiliary features such as zippers, tear notches, one-way degassing valves, and hanging holes. Barrier levels, dimensions, and composite structures can be customized to meet specific requirements. All pouches comply with relevant industry safety and regulatory standards, offering long-term, reliable protection for high-value products.

WHY CHOOSE US?
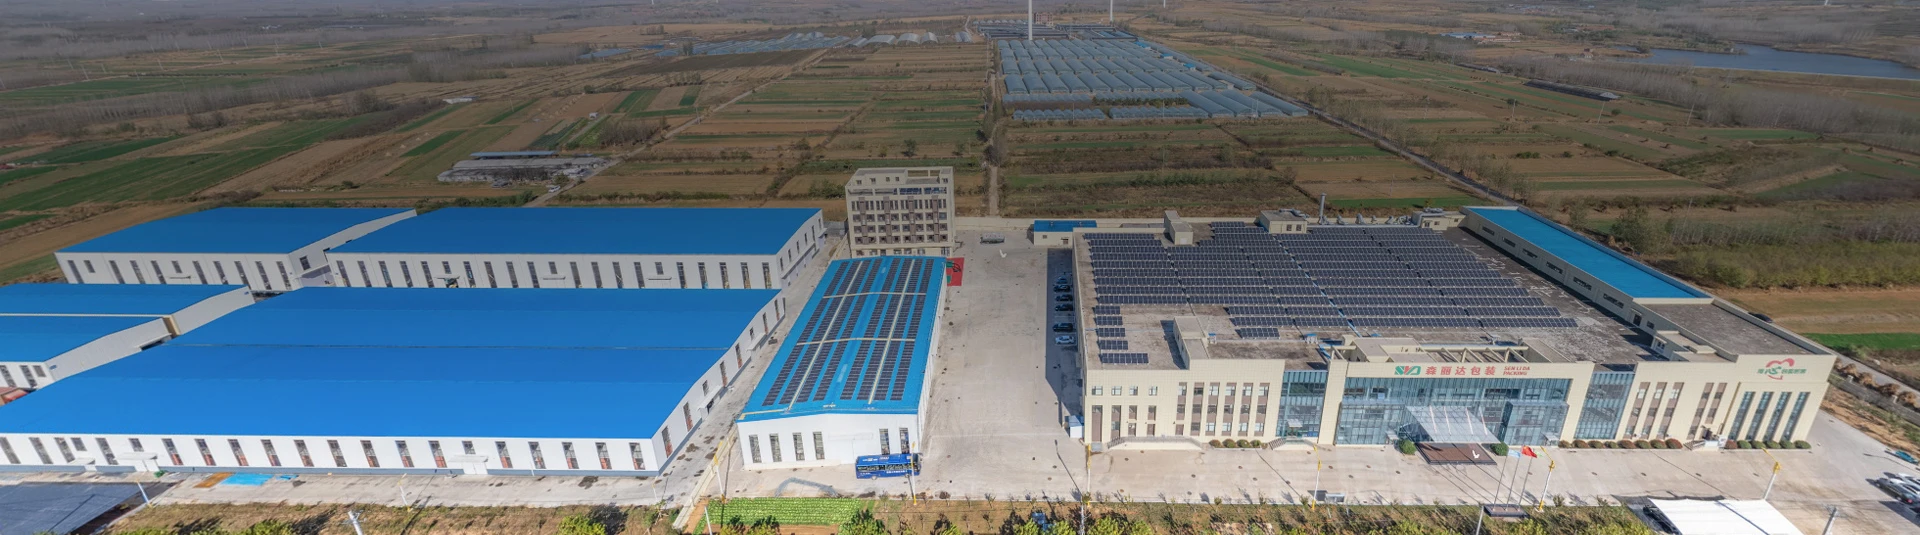
Leveraging a fully integrated, intelligent production setup combined with mature lean manufacturing management, we achieve large-scale, highly stable production capacity. Functional composite film rolls can be produced at up to 30 tons per day, while finished pouches can reach a daily output of 2 million units.

We are always at your service when you need
This ample production capacity allows us to accommodate everything from small-scale sampling and pilot orders to large-volume orders of hundreds of thousands or millions of units, providing global customers with efficient, reliable, and on-time delivery.
Years of Experience
Production Area
Daily Output
Annual Output Value
FREQUENTLY ASKED QUESTIONS
1. What does "high-barrier" mean for back seal pouches, and which core performance indicators should I pay attention to?
+
-
High-barrier back seal pouches refer to pouches with composite structures that provide strong resistance against oxygen, water vapor, and light. Key indicators include OTR (oxygen transmission rate) and WVTR (water vapor transmission rate). Different material laminations deliver different barrier levels. We can provide actual test data for your reference when selecting materials for your products.
2. What material combinations are available for high-barrier back seal pouches? What is the difference between aluminum-plated and full-aluminum-foil options?
+
-
Common high-barrier structures include PET/VMPET/PE, PET/AL/PE, NY/AL/CPP, and other multi-layer composites. Aluminum-plated pouches offer a metallic look with moderate barrier and lower cost. Full-aluminum-foil pouches offer superior oxygen, moisture, and light-blocking performance yet are completely opaque. You can choose based on your shelf-life target and whether you need a product viewing window.
3. Will high-barrier back seal pouches lose their barrier effect after heat-sealing or during long-distance transportation?
+
-
Proper composite and heat-seal processing will not damage the barrier layer. However, sharp-edged contents, excessive bending, or heavy friction during transit may cause tiny pinholes and weaken barrier performance. We can adjust film toughness and layer structure for heavy-weight or sharp-content goods to reduce pinhole risks.
4.Are high-barrier back seal pouches suitable for both dry and oily, high-moisture products? Are there any restrictions?
+
-
They work well for dry food, nutraceuticals, and pet food. For high-oil or high-moisture goods, you need to match the right inner sealing layer. Standard PE layers may swell under long-term contact with grease; we recommend modified CPP materials for oily contents. Please inform us of your product's oil and moisture level so we can recommend a suitable structure.
5. Can high-barrier back seal pouches be customized with features such as zippers, valves or tear notches? Will these fittings compromise the overall barrier performance?
+-
Yes, zippers, one-way degassing valves, and easy-tear notches are all supported. Zippers and valves are potential weak points for the barrier system. We adopt high-barrier matching accessories and optimize the sealing process to minimize performance loss. If maximum shelf-life is critical, we will evaluate accessory impacts and suggest the most practical solution.
Hot Tags: high barrier back seal pouches, China high barrier back seal pouches manufacturers, suppliers, factory, Aluminum Foil Back Seal Pouch, Back Seal Pouches for Pet Food, fin seal pouches, Food Grade Back Seal Pouches, High Barrier Back Seal Pouches